SMT Assembly Cost per Point: Pricing, Cost Drivers and Quotes
Understand SMT assembly cost per point, its limits, and the real drivers behind prototype, low-volume, and high-volume PCBA pricing and optimization choices.
Get Your PCB Quote!
Table of Contents
- Qual a faixa de preço esperada para montagem SMT?
- Resposta rápida: o que significa custo por ponto na montagem SMT?
- Modelo completo de custo de montagem SMT
- Por que a precificação por ponto tem limites
- Como a complexidade dos componentes e do processo altera o custo da montagem SMT
- NRE, estênceis, dispositivos de fixação, testes e fornecimento de componentes
- Diferenças de custo entre protótipos, produção em baixo volume e produção em alto volume na fabricação de sistemas SMT
- Otimização de custos que não gera risco de qualidade
- O que incluir em uma solicitação de custo de montagem SMT
- Perguntas frequentes
- Contexto de fontes e padrões
Table of Contents
- Qual a faixa de preço esperada para montagem SMT?
- Resposta rápida: o que significa custo por ponto na montagem SMT?
- Modelo completo de custo de montagem SMT
- Por que a precificação por ponto tem limites
- Como a complexidade dos componentes e do processo altera o custo da montagem SMT
- NRE, estênceis, dispositivos de fixação, testes e fornecimento de componentes
- Diferenças de custo entre protótipos, produção em baixo volume e produção em alto volume na fabricação de sistemas SMT
- Otimização de custos que não gera risco de qualidade
- O que incluir em uma solicitação de custo de montagem SMT
- Perguntas frequentes
- Contexto de fontes e padrões
“How much does SMT assembly cost per point?” is a useful first question, but it is not enough to predict the cost of a finished PCBA. In most quotations, a point means one SMT placement, yet suppliers may count points differently: a component body, a placement operation, a pad group, or an operation that also includes inspection. Two boards with the same placement count can therefore have very different total costs.
The practical way to budget is to separate variable placement cost from everything that makes a specific build difficult: component procurement, package type, board sides, BGA inspection, through-hole work, NRE, stencils, fixtures, test, yield risk, and shipment. This guide explains the cost model and how to reduce cost without quietly increasing reliability risk.
Price per point can be useful for an early comparison, but it cannot represent the complete manufacturing scope. Buyers should compare component packages, board sides, inspection, testing, sourcing and production quantity before selecting a supplier. Review our SMT assembly services for supported processes and production capabilities.
What price range should you expect for SMT assembly?
If you need a planning number, start with the ranges below—not with a single headline rate. These are published supplier estimates and one public calculator example, so they are useful price anchors rather than a universal market price. Geography, currency, order quantity, component availability, quality requirements, and what the supplier includes can move the final quote substantially.
| Quote item | Published or indicative range | How to read it |
| Common resistor/capacitor placement | $0.001–$0.01 per placement | Supplier-reported range for simple parts; excludes most fixed costs. |
| Standard IC placement | $0.01–$0.05 per placement | Indicative supplier range; package, feeder setup, and volume matter. |
| Fine-pitch, QFN, or BGA placement | $0.05–$0.20+ per placement | Supplier-reported range; inspection and process-control requirements may be extra. |
| SMT setup/NRE | $150–$500 per order | Published supplier estimate for typical stencil, programming, and fixture work; scope varies. |
| Inspection and test | $0.50–$5.00 per board | Published supplier estimate; AOI, X-ray, ICT, and functional test are different services. |
| Small public calculator example | $20.75 per board; $207.50 for 10 boards | Example configuration with 100 SMT and 10 THT, a $30 stencil, $32 placement, and $0.50 testing; not a universal quote. |
The placement, setup, inspection, and calculator figures above come from different published sources and should not be added together blindly. The supplier-reported placement ranges are discussed by TXJ PCBA; the setup and inspection estimates, plus an assembly-only example for a 200-component board at 100 units, are published by Atlas PCB. The 10-board example is from the PCBCostCalculator public calculator. Treat them as quote-screening references, not as a promise from OrinewPCB or a substitute for a BOM-based quotation.
For a simple planning illustration, 200 ordinary SMT placements at $0.01–$0.05 would represent about $2–$10 of variable placement work per board. If a $150–$500 setup charge is spread across 100 boards, that adds another $1.50–$5 per board before the PCB, components, inspection, test, shipping, and any THT work. This arithmetic is only a budgeting example; the supplier must confirm how it counts a point and what its rate includes.
Need PCB Manufacturing or Assembly?
Get a free quote within 24 hours. We specialize in prototype-to-production PCB/PCBA for hardware teams worldwide.
Quick answer: what does SMT assembly cost per point mean?
An SMT point rate is usually a line-item estimate for placing one surface-mount component. It is most useful when comparing similar boards built with the same process, volume, panel format, and quality requirements. It is not a complete PCBA price.
Ask each supplier to state exactly what the point rate includes. A meaningful quote should clarify whether the rate covers programming, feeder setup, solder paste, reflow, AOI, handling of odd-form parts, double-sided placement, BGA-related inspection, and any minimum assembly charge.
| A point rate can help estimate | A point rate cannot reliably predict by itself |
| Relative placement effort for comparable SMT-only boards | Component cost, engineering setup, stencil cost, test fixtures, BGA X-ray, THT insertion, rework risk, or shipping |
| The effect of a large increase in ordinary component placements | The cost effect of changing from a simple 0603 resistor to a fine-pitch BGA, connector, press-fit part, or double-sided process |
| Variable production cost after a process is already validated | Prototype or low-volume cost, where fixed setup and engineering charges dominate |
The decision rule is simple: use a per-point number as one input, then review the full cost breakdown before comparing suppliers. A lower point rate can be offset by higher NRE, test, sourcing, or special-process charges.
The complete SMT assembly cost model
For planning purposes, total PCBA cost can be viewed as the sum of five groups:
| Cost group | What it includes | Why it changes |
| Board and components | Bare PCB, purchased parts, approved alternates, incoming inspection, and component attrition. | Supplier availability, purchase quantity, lead time, lifecycle risk, and the BOM’s approved manufacturer list. |
| Assembly operations | Stencil printing, placement, reflow, AOI, hand work, cleaning, and rework allowance. | Placement count, package mix, sides assembled, panel format, and required process controls. |
| One-time engineering | CAM/DFM review, programming, first-article preparation, and production documentation. | Revision maturity, data quality, build complexity, and whether a validated program already exists. |
| Tooling and test | Stencils, pallets, selective-solder tooling, ICT fixtures, functional-test fixtures, and test development. | Board geometry, test coverage, expected volume, and whether tooling can be amortized across future builds. |
| Logistics and quality | Packaging, traceability, inspection, certificates, export handling, and shipping. | Destination, handling needs, required records, and the product’s reliability or regulatory requirements. |
This model is also the bridge for the article being redirected here: cost optimization is not “find the lowest placement rate.” It is removing avoidable setup, sourcing, and rework cost while keeping the material and process controls appropriate for the product.
Why pricing by point has limits
Point pricing works best for stable, repeatable SMT jobs. It becomes weak when a component changes the process rather than merely adding another placement.
Examples include a fine-pitch BGA that needs X-ray or tighter process validation, a connector that requires selective soldering, a double-sided board that adds a second placement and reflow sequence, or a board with too many unique components for a fast feeder setup. These are not “just more points.” They change programming, setup, inspection, or yield exposure.
The most useful quote separates ordinary placement points from exception groups. This lets the buyer see whether the cost is caused by volume, a component decision, a test requirement, or a supplier’s minimum charge.
How components and process complexity change SMT assembly cost
Component count and unique part count
More placements normally add variable cost. More unique part numbers can also increase feeder preparation, material handling, traceability, and substitution review. A 500-point board built from a repeatable set of passives may be easier to run than a lower-point board with many unique reels, tightly controlled alternates, or short-life components.
Package type and fine-pitch parts
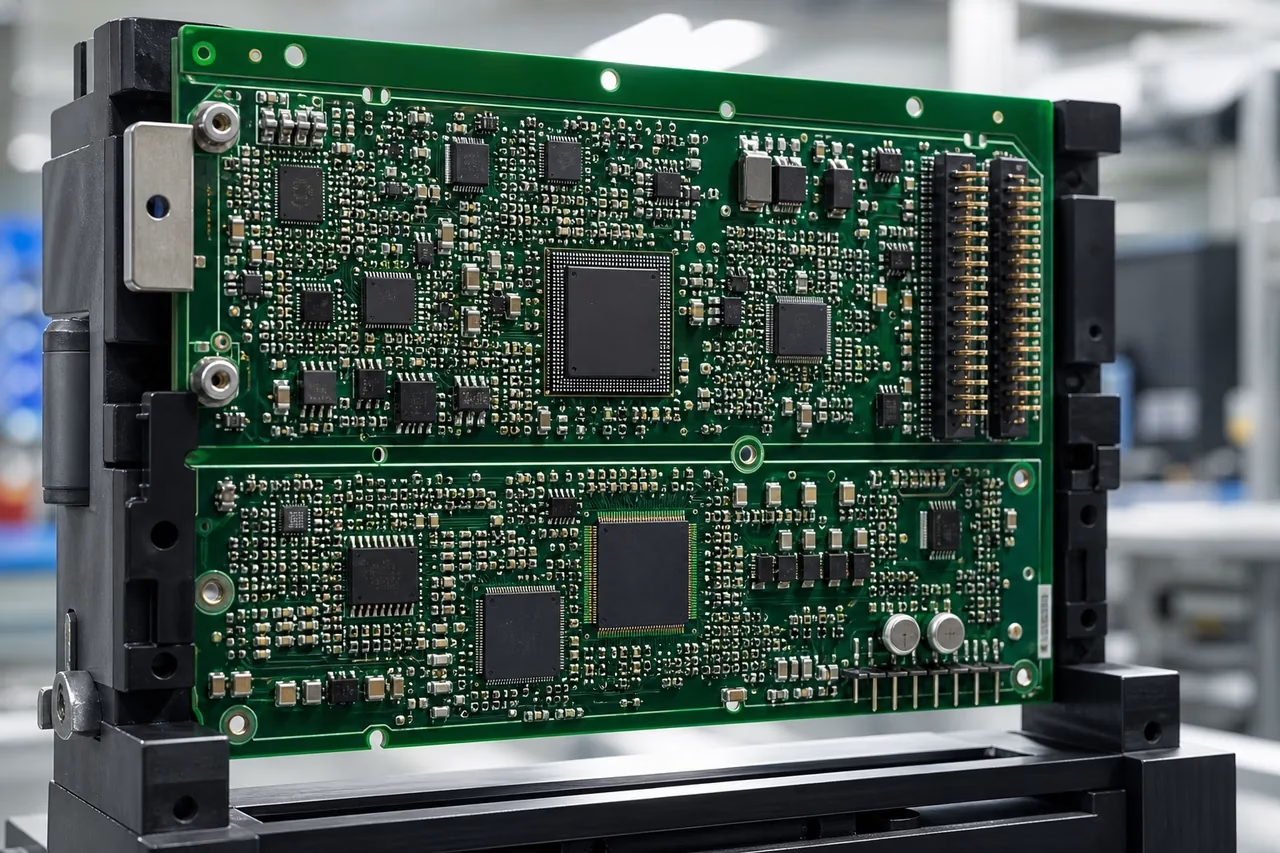
Standard passives and common IC packages are usually straightforward when the footprint, stencil, and placement data are correct. Fine-pitch QFNs, BGAs, bottom-terminated components, and unusual packages can raise cost because they may need tighter paste control, more careful profile development, x-ray sampling, or higher rework risk.
BGA inspection and yield risk
A BGA changes the inspection plan because its solder joints are hidden below the package body. AOI can inspect visible placement and surrounding workmanship, but it cannot see the internal ball array. Depending on the product and agreed quality plan, the build may need X-ray for first article, sampling, or targeted investigation. That requirement should be quoted as its own item, not hidden in a generic per-point rate.
Double-sided SMT assembly
Double-sided assembly can add a second print, placement, and reflow sequence. It may also constrain component selection and board support during reflow. Do not estimate a double-sided board by simply doubling a single-side point price; confirm the panel design, side sequence, adhesive or reflow strategy, and parts that may be exposed to the second thermal cycle.
THT and mixed-technology work
Through-hole components are usually priced separately from SMT points. Manual insertion, lead forming, wave or selective soldering, press-fit operations, and mechanical hardware each create different labor, tooling, and inspection requirements. For an accurate mixed-technology quote, identify every THT group and its required soldering method in the assembly drawing.
NRE, stencils, fixtures, test, and component sourcing
Fixed costs are the reason a small prototype can look expensive per board even when its placement count is low. They should be visible rather than blended into an unexplained assembly rate.
| Cost item | What it pays for | How to manage it responsibly |
| NRE | DFM review, CAM preparation, BOM normalization, program creation, and first-article setup. | Release complete Gerber, BOM, centroid, assembly drawing, and revision-controlled notes together. Avoid late file changes after programming begins. |
| Stencil | Apertures matched to the solder-paste design and assembly side. | Use a reviewable paste layer and confirm whether one or more stencils are required for the build sequence. |
| Fixture or pallet | Board support, selective/wave solder protection, ICT contact, or functional-test repeatability. | Amortize durable tooling only when the expected production volume supports it. Do not remove a needed fixture merely to lower a prototype quote. |
| Test development | Test-point planning, fixture design, programming, limits, and debug of ICT or functional test. | Match test depth to product risk. A defined test strategy can reduce field and rework cost even when it adds an upfront charge. |
| Component sourcing | Distributor purchasing, alternates review, incoming inspection, traceability, and handling of shortages. | Approve alternates in advance and consolidate passives where technically safe. Do not substitute critical components on price alone. |
For prototypes, the goal is not to eliminate every fixed cost. It is to spend on the engineering checks that prevent an avoidable respin. For production, the goal is to spread validated tooling and programming across enough boards that unit cost falls without losing process control.
Prototype, low-volume, and high-volume SMT cost differences
The same BOM can produce very different unit prices at different volumes because fixed work is divided across a different number of boards and the production method changes.
| Build stage | Typical cost pattern | Best cost decision |
| Prototype | NRE, stencil, setup, and small-quantity component purchasing dominate the cost per board. | Prioritize DFM, component availability, and a test plan that teaches the team something before the next revision. |
| Low-volume or pilot build | Setup is spread across more boards, but changeovers and mixed part demand still matter. | Lock the BOM and panel strategy, validate yield, and decide which fixtures or tests should carry into production. |
| High-volume production | Validated programs, panel use, bulk procurement, and amortized tooling reduce the unit cost. | Protect supply continuity, test coverage, traceability, and process capability instead of chasing a lower point rate alone. |
There is no universal quantity at which a project “becomes high volume.” The right break point depends on board size, component demand, line utilization, tooling cost, and product lifetime. Ask for pricing at the quantities you actually expect to order, including a realistic pilot quantity, rather than comparing one prototype quote with a theoretical production rate.
Cost optimization that does not create quality risk
The best cost reductions remove repeated work, procurement friction, and design ambiguity. They do not simply reduce inspection, eliminate test points, or replace approved parts with unverified alternatives.
- Consolidate passive values and packages where the circuit allows it, reducing unique part numbers and feeder changeover.
- Select components with stable supply and approved alternates before the build, not after a shortage delays production.
- Design a panel and tooling approach with the assembler before release; panel rails, fiducials, breakaway method, and support can affect placement and depanelization cost.
- Make the BOM, Gerber files, centroid data, paste data, assembly drawing, and test notes agree on the same revision.
- Use the required inspection and test evidence for the risk. Cutting X-ray, AOI, ICT, or functional test without changing the product risk does not reduce the cost of a defect; it only moves the discovery point later.
- Avoid unnecessary special processes, but keep the processes a component package or end-use requirement genuinely needs.
OrinewPCB can review these inputs as part of a PCB assembly quote and DFM review. For broader production planning, see the PCB assembly process and volume selection guide and the assembly testing guide.
What to include in an SMT assembly cost request
An actionable request gives the manufacturer enough information to separate placement cost from the real cost drivers.
- Gerber or ODB++ data, including the paste layers and board outline.
- BOM with manufacturer part numbers, quantities, approved alternates, and customer-supplied parts identified.
- Centroid or pick-and-place data with the correct side, rotation convention, and reference designators.
- Assembly drawing showing polarity, special placement notes, THT groups, hardware, and side sequence.
- Required quantity for prototype, pilot, and projected production builds.
- BGA, fine-pitch, double-sided, selective-solder, conformal-coating, and cleaning requirements.
- Inspection and test requirements, including X-ray, AOI, ICT, functional test, programming, and record retention.
- Shipping destination, required delivery date, and any packaging or traceability requirement.
Frequently asked questions
Is SMT assembly cost per point the same as the total PCBA cost?
No. It normally represents only placement effort. Total PCBA cost also includes the bare PCB, components, NRE, stencils, test, inspection, tooling, logistics, and special processes.
Do BGAs cost more than standard SMT components?
They can. The placement count alone may be one point, but the package can require paste-process control, profile validation, X-ray inspection, and more difficult rework. Ask for BGA handling and inspection as separate quote items.
Why is a prototype more expensive per board?
One-time engineering, stencil, setup, and small-quantity purchasing are divided across few boards. The unit price normally falls as validated setup and tooling are spread across more units.
Can I reduce cost by removing test or inspection?
Only if the removed step does not provide necessary evidence for the product’s risk. A test strategy should be selected deliberately; removing it to reduce a quotation can create a much higher downstream rework or field-failure cost.
Sources and standards context
- IPC J-STD-001J: scope for soldered electronic assembly materials, methods, and acceptance requirements.
- IPC overview of J-STD-001J and IPC-A-610J: distinction between process requirements and post-assembly acceptability.
Get Quote Free